Home > About Us
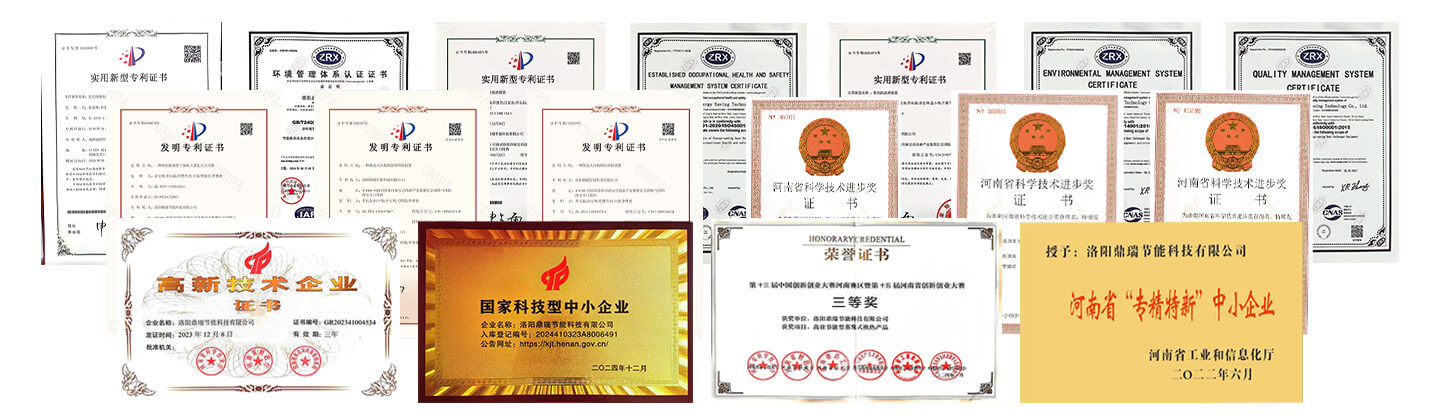
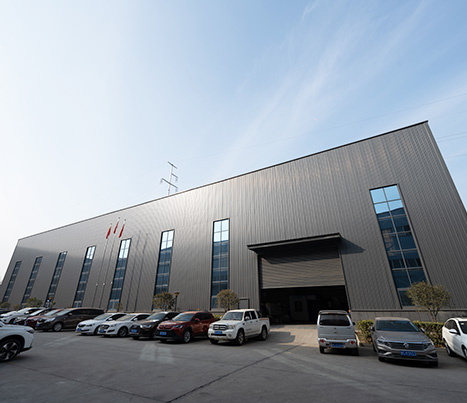
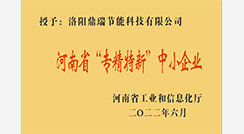
Established in 2018 and located in the Luoxin Industrial Cluster of Luoyang City, Luoyang Dingrui Energy Saving Technology Co., Ltd. has rapidly developed into an innovative benchmark in the field of industrial heat exchange and energy conservation & environmental protection. The company is recognized as a National High-tech Enterprise, a National Sci-tech SME, and, notably, has been designated as a Henan Provincial “Specialized, Refined, Unique, and New” SME. These accolades signify the authoritative recognition we have achieved on our path of technological innovation and specialized development.
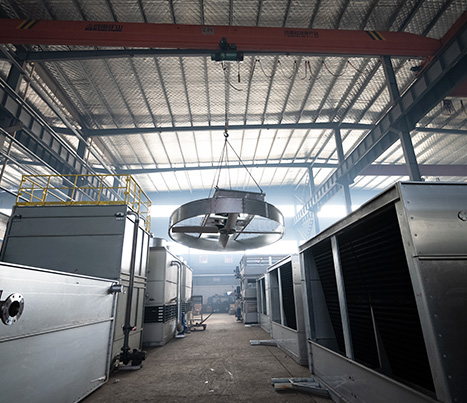
The company specializes in providing efficient and reliable industrial heat exchange solutions and environmental protection equipment for pillar industries of the national economy, including power generation, metallurgy, petrochemicals, coal chemical, and refrigeration. Our comprehensive product portfolio encompasses evaporative heat exchange equipment, air-cooled heat exchange equipment, and innovative hybrid products that combine both technologies. Through independent R&D and continuous innovation, we are dedicated to helping customers reduce energy consumption, decrease water usage, enhance system stability, and achieve significant economic and environmental benefits.
Founded in 2018, it is recognized as a national high-tech enterprise in China.
Luoyang Dingrui specializes in the research, development, design, production and service of industrial conversion and energy-saving & environmental protection equipment.
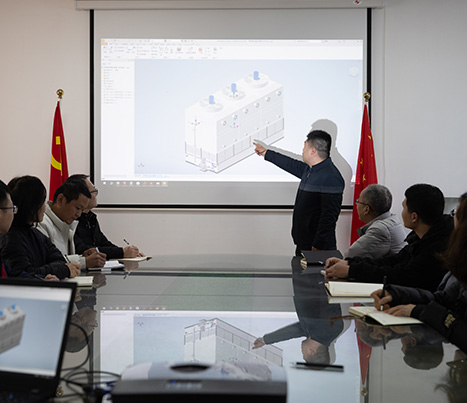
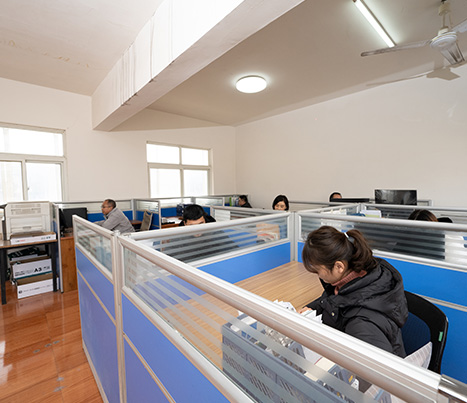
(1) Provide one-on-one engineer consultation for different industries (such as high-temperature working conditions in the chemical industry, low-noise requirements in electronics factories, and load heat dissipation in power plants) to analyze customers' actual heat dissipation needs (such as hourly heat dissipation capacity, inlet water temperature, and water quality conditions).
(2) Issue free non-standard customized schemes (such as square/circular cooling towers, cross-flow/counter-flow structures, and anti-corrosion material upgrades), with technical parameter sheets, 3D renderings, and cost estimates attached, allowing customers to clearly understand "why this model is chosen".
(1) Dispatch a technical team to conduct on-site surveys of the installation site (such as space dimensions, load-bearing capacity, and water/power source locations), and evaluate the adaptability of the customer's existing production process to the cooling tower (such as whether it needs to be linked with the original cooling system).
(2) Predict potential issues (such as installation difficulties caused by narrow sites and equipment corrosion risks in high-temperature and high-humidity environments), and avoid them in the scheme in advance to prevent customers from reworking later.
(1) Commit to a clear delivery cycle (e.g., 7-15 working days for standard models and 30-45 working days for customized models), and provide an order progress inquiry channel (such as real-time synchronization of production and logistics status by a dedicated customer service representative) to prevent customers from "delaying production due to waiting for equipment".
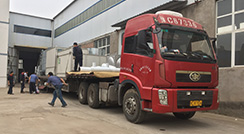
(2) Offer door-to-door delivery (including unloading service), and provide dedicated logistics for large cooling towers to ensure no collision during equipment transportation (with transportation insurance attached, and compensation for damage).
The core team members began their work in the field of industrial heat exchange. They were the first to apply evaporative heat exchangers to steam turbine exhaust systems. This achievement earned them a provincial-level award, specifically the National Science and Technology Progress Award.
The company was established. We implemented management systems for Quality, Environment, Health, and Safety in accordance with ISO standards and obtained the corresponding certifications.We sold our first cooling tower.
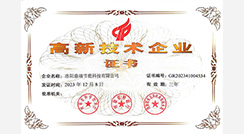
Thanks to our advanced technical concepts and excellent product quality, the company was recognized as a National High-Tech Enterprise.
We obtained certification for our intellectual property management system, which is designed to systematically manage and protect our innovative achievements.
We participated in the development of industry group standards, including "Air-Cooled Condenser Tube Bundles for Petrochemical Steam Turbines" and "Evaporative Condensers for Steam Turbines."
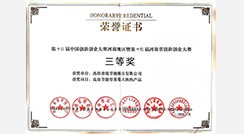
We took part in the 13th China Innovation and Entrepreneurship Competition, where our project "Efficient and Energy-Saving Evaporative Heat Exchangers" won the third prize in Henan Province. Our number of patents has now exceeded 30. The company has also been recognized as a National Tech-based SME.
At DRTECH, you can find the perfect solution that meets your specific process requirements.
This is made possible by our skilled and comprehensive R&D team. Engineers always account for more than 20% of the company's employees, with expertise spanning Thermodynamics and Hydraulics, Process, Mechanical, Electrical, Instrument and Control, Piping, and Structural engineering. The engineering team is proficient in various design software and can deliver professional and accurate technical services in a fast and efficient manner.
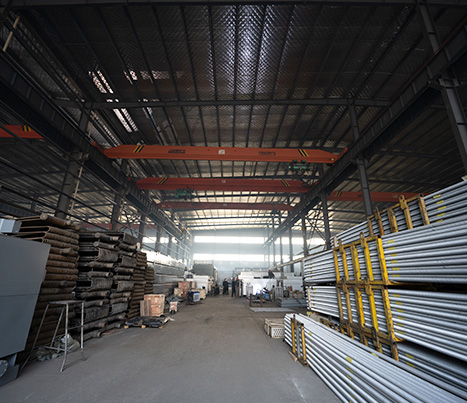
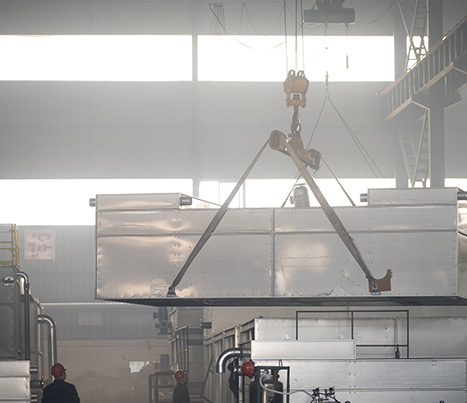
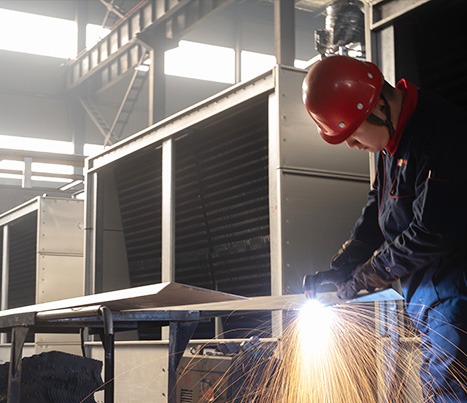
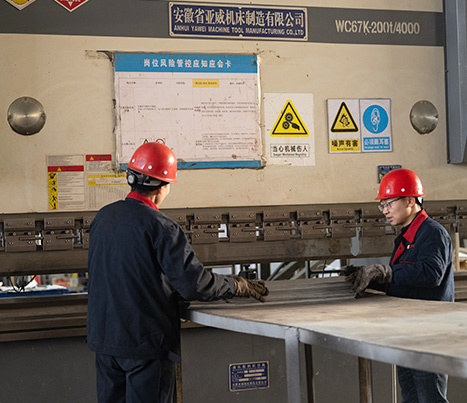
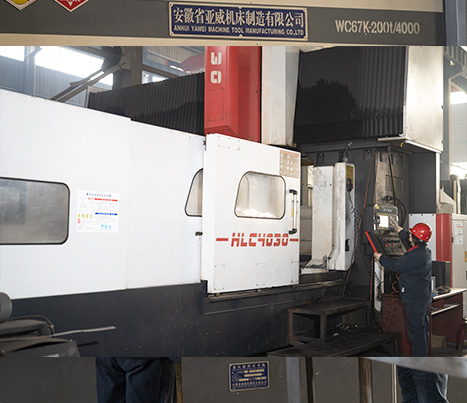
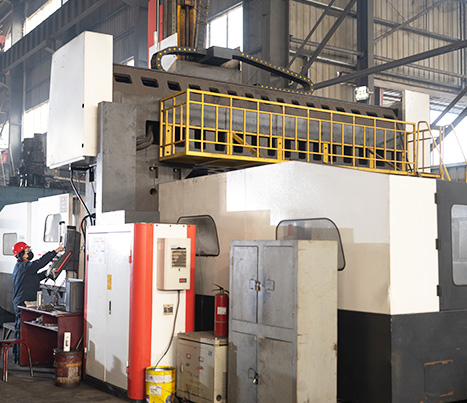
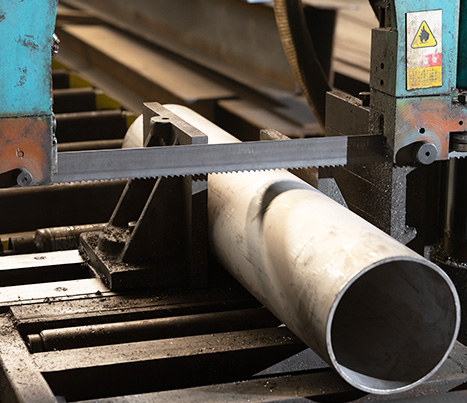
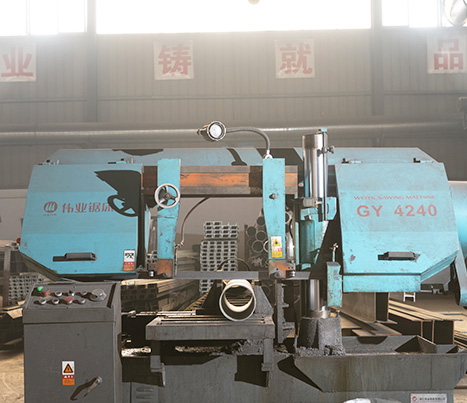
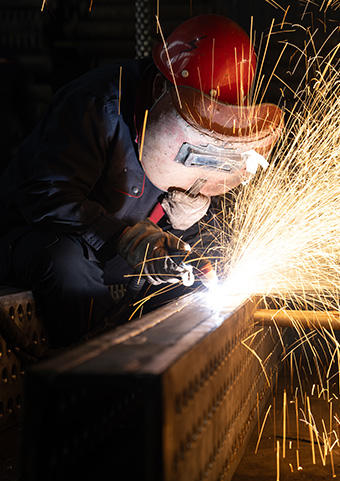
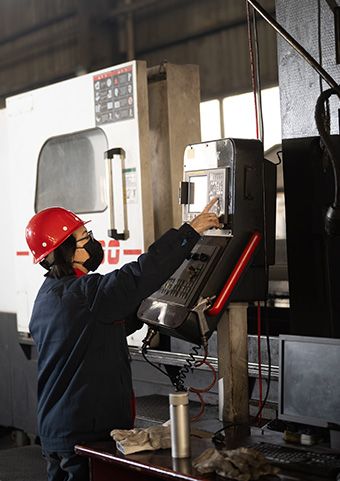
The reliability and durability of equipment are always our top priority. To ensure this, we have established complete production lines, adopted advanced intelligent manufacturing techniques, and implemented stringent quality control standards.
The company is recognized as a National High-tech Enterprise, a National Sci-tech SME, and, notably, has been designated as a Henan Provincial "Specialized, Refined, Unique, and New" SME. These accolades signify the authoritative recognition we have achieved on our path of technological innovation and specialized development.